Business
Stop Assembly Misfits: Fix Five GD&T Drawing Errors Before Release

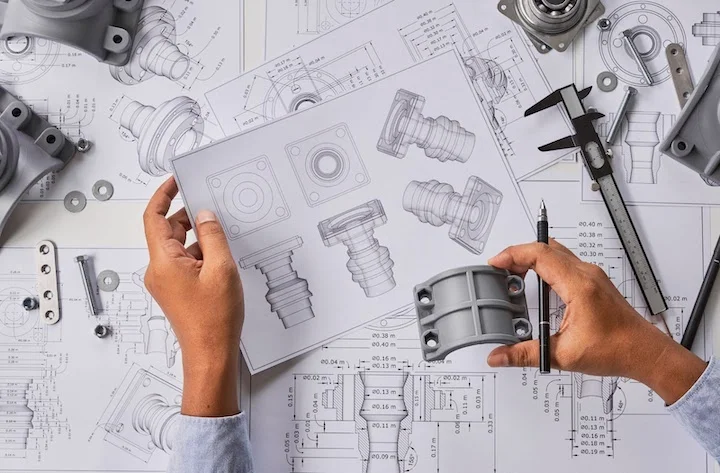
Assembly problems often trace back to how engineers applied geometric dimensioning and tolerancing (GD&T) when the drawing or model left engineering. A bolt circle that “should fit” but requires pry bars, a plastic housing that rocks on its mating surface, or a bracket that twists when torqued are not random shop floor surprises. They are predictable outcomes of unclear datum schemes, missing material condition modifiers, vague pattern definitions, and inspection that does not match the stated tolerances—addressing a handful of recurring GD&T mistakes before release prevents scrap, rework, and supplier disputes.
- Choose functional datums, not convenient ones.
Common mistake: setting primary, secondary, and tertiary datums from the easiest faces to probe rather than the features that locate the part in the real assembly. If the part assembles on a pilot bore and a machined shoulder, those should form the primary and secondary datum features. Using two random flat pads because they are “stable” on a surface plate creates a datum reference frame that disagrees with the mating condition, so positional tolerances on holes and slots do not reflect how the part is actually constrained.
Consequence and fix: when datum features represent the assembly interfaces, tolerance zones line up with function. For example, a gearbox cover located by its spigot (primary datum A) and bolt circle (secondary datum B) will keep seal compression consistent. If you use flat pads instead, bolt holes can be in tolerance while the spigot runs out of position. Define datum simulators (e.g., a fixed spindle for the bore, hard points for shoulders), use datum targets if needed on castings, and call out modifiers such as MMB when fasteners or clamps allow shift during assembly. Teams often collect examples from standards bodies and from public engineering sites, including AEC Inc., to help align on a datum strategy that mirrors how parts actually seat and locate.
- Specify material condition on position when fasteners are involved.
Common mistake: leaving positional tolerances “RFS by default” on clearance holes, dowel holes, or slots used with bolts. Without maximum material condition (MMC), you give up useful bonus tolerance that exists when features depart from maximum material. You also block functional go gages for quick verification and force slower coordinate measuring machine (CMM) setups, even for straightforward hardware.
Consequence and fix: With position at MMC, a bolt hole gets additional allowable positional error as its diameter grows away from its minimum size. This bonus tolerance reflects real-world assembly freedom and reduces nonconformances that do not affect fit. A sheet metal bracket with 10 mm clearance holes for M8 bolts is a classic case: position at MMC enables simple fixed gaging and faster acceptance while still protecting clamp load. Save “RFS” for fits where size change does not buy functional leeway, such as press fits or precision datums. When using slots, consider a projected tolerance zone for tall stacks so bolt tilt does not collide with mating features.
- Control hole patterns so parts move as one.
Common mistake: tolerancing each hole in a pattern individually with a single segment position callout, then discovering the pattern breathes during assembly. If the holes relate loosely to each other, a part can meet each feature’s tolerance and still bind because the pattern center drifts or the pattern warps.
Consequence and fix: composite position and pattern locating schemes separate two needs. The upper segment locks the pattern to the datum reference frame (PLTZF), controlling pattern drift as a whole. The lower segment tightens how features relate within the group (FRTZF), controlling neighbor spacing and orientation. On a five-hole valve body, composite position stops the bolt circle from shifting while keeping bolt-to-bolt spacing tight for gasket load. If design requires a pattern to float together for assembly clearance, use a single segment with simultaneous requirement across patterns that must act in unison. Document whether patterns are separate or simultaneous to avoid unexpected “pattern shift” on the shop floor.
- Use profile and orientation deliberately, not as a catch-all.
Common mistake: throwing profile of a surface around complex geometry without stating what profile controls and why. Another is using profile to imply location when a true position or orientation control tied to datums would be more readable. These shortcuts make it hard for machinists and inspectors to decide where to set up and how to verify, especially on freeform surfaces or molded parts.
Consequence and fix: profile excels at controlling shape and size relative to a datum reference frame, but it must be paired with the right datums and tolerance zones. For an injection-molded housing, use profile relative to the mounting plane and locator bosses to keep cosmetic surfaces within a band while preserving latch function. For cylindrical bores that must align, a position or runout control coupled to functional datums is clearer than a blanket profile. Consider unequal profile distribution to leave more stock on cosmetic faces and less near sealing features, and avoid all-around symbols when only a subset of edges needs control. Clear feature-control framing reduces ambiguity and CMM reprogramming time.
Define inspection and data handoff on the drawing and model
Common mistake: releasing PMI in a model-based definition (MBD) that suppliers cannot read, or not stating how features should be verified. This leads to CMM alignments that don’t match the datum reference frame, gage designs that miss material condition, and PPAP/FAI reports that cannot be reconciled with engineering intent.
Consequence and fix: specify the inspection alignment explicitly. If datums A|B|C define the setup, say so and avoid alternate datum precedence unless intentional. Where position uses MMC, allow functional go gages or projected tolerance zones and note when a functional thread gage is required. State the authority file (drawing PDF or CAD model) and version, and confirm your STEP AP242 or native CAD export preserves GD&T symbols, composite callouts, and datum targets. Involve quality early to align sampling, gage R&R expectations, and reporting formats. A realistic example: a tall standoff with a threaded hole might pass CMM when aligned to a flat that is only secondary in the assembly. Calling out a projected tolerance zone and clarifying datum order prevents false accepts that later cause cross-threading.
The most reliable assemblies start long before torque wrenches hit the line. Datums that mirror mating features, position with the right material condition, pattern controls that distinguish “where” from “how together,” and inspection plans that match the drawing all translate design intent into parts that fit. Apply these choices while models and drawings are still fluid, review them with manufacturing and quality, and test them with a quick gage or CMM mockup. Catching one ambiguous feature control frame in review is cheaper than discovering during PPAP that a housing rocks, a bolt pattern binds, or a bore aligns only on paper.

What Models Does ImagineArt Actually Run?

BadSeed Tech Carpio Explained: What This Collab Actually Is

Metronidasool Fact-Checked: The Medication Behind This Spelling

Who Is Nicole Saphier? The Amazing Life Story of Dr Paul Saphier’s Wife

Who Is Alisa Earle? The Amazing Life Story of Alix Earle’s Mother

Who Is Jordan Foxworthy? The Untold Life Story of Jeff Foxworthy’s Daughter

Who Is Jaisal Andrews? Inside the Life of Naveen Andrews’ Son

Who Is Saffron Le Bon? The Untold Life Story of Benjamin Compston’s Wife

Who Is Tanja Rosner? The Untold Life Story of Tate McRae’s Mother

Voozon.com Explained: What It Really Is Behind the “Knowledge Platform” Label

Who Is Sue Johnston? The Remarkable Life Story of Joel Palmentor’s Mother

Who Is Kerri Browitt Caviezel? The Inspiring Life Story of Jim Caviezel’s Wife
-
 Celebrity2 months ago
Who Is Jaisal Andrews? Inside the Life of Naveen Andrews’ Son
-
 Celebrity2 months ago
Who Is Saffron Le Bon? The Untold Life Story of Benjamin Compston’s Wife
-
 Celebrity2 months ago
Who Is Tanja Rosner? The Untold Life Story of Tate McRae’s Mother
-
 Software4 weeks ago
Voozon.com Explained: What It Really Is Behind the “Knowledge Platform” Label
-
 Celebrity2 months ago
Who Is Sue Johnston? The Remarkable Life Story of Joel Palmentor’s Mother
-
 Celebrity2 months ago
Who Is Kerri Browitt Caviezel? The Inspiring Life Story of Jim Caviezel’s Wife
-
 Celebrity2 months ago
Who Is Otelia Cox? The Remarkable Life Story of Tony Cox’s Wife
-
 Software4 weeks ago
Bynethi Com Explained: What to Verify Before Trusting This Site